KHTS Radio Santa Clarita Radio – Santa Clarita News

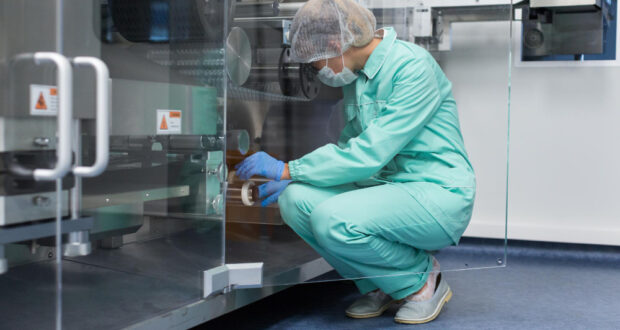
Modern medicine depends on the ability to maintain drug stability from manufacture to patient use. Many pharmaceutical compounds, particularly biological products, are sensitive to heat, moisture, and time. Consequently, freeze-drying has become a cornerstone preservation technique that enables long-term storage without compromising therapeutic value. Lyophilisation, when properly controlled, protects molecular integrity while simplifying transport and distribution.
In practice, pharmaceutical manufacturers rely on advanced cold-chain infrastructure to ensure process consistency. The integration of specialized refrigeration systems plays a decisive role because a lyophilizer for a pharmaceutical production environment must operate with high reliability, stable temperature control, and accessible maintenance support to safeguard product quality across every batch. This operational precision is not merely technical — it is fundamental to patient safety and regulatory compliance.
The Science Behind Pharmaceutical Freeze-Drying
Understanding Sublimation in Drug Preservation
Lyophilisation works by removing water from frozen products through sublimation, meaning ice transitions directly into vapour under reduced pressure. This mechanism is especially valuable for pharmaceuticals because water often drives chemical reactions that degrade active ingredients. By eliminating moisture, the process effectively slows down deterioration pathways such as hydrolysis or oxidation.
Moreover, freeze-drying preserves the physical structure of complex molecules. Proteins, peptides, and vaccines often require delicate handling since their biological activity depends on maintaining a precise three-dimensional configuration. By stabilizing them in a dry state, lyophilisation helps maintain efficacy until the product is reconstituted before administration.
Why Stability Matters for Modern Therapies
Pharmaceutical formulations can broadly be categorized into small-molecule drugs and biologics. While many traditional compounds tolerate standard storage conditions, biologics often demand specialized preservation. Freeze-drying bridges this gap by enabling long shelf life without continuous refrigeration in some cases.
Key stability benefits include:
- Reduced chemical degradation caused by moisture
- Enhanced resistance to temperature fluctuations
- Preservation of molecular conformation
- Simplified storage and transport logistics.
These advantages explain why lyophilisation is frequently used for vaccines, injectable therapies, and diagnostic reagents.
Stages of Lyophilisation in Pharmaceutical Production
Freeze-drying is not a single-step procedure but rather a carefully managed sequence of phases. Each stage influences product quality, making process optimisation essential.
Primary Stages of the Process
- Freezing: The solution is cooled to form solid ice crystals, which define the material’s porous structure.
- Primary drying (sublimation): Under vacuum, ice converts to vapor, leaving behind a stable matrix.
- Secondary drying (desorption): Remaining bound moisture is removed to achieve final stability.
Precise control of temperature and pressure during these phases ensures uniform drying while preventing collapse or structural damage.
Applications Across Pharmaceutical Categories
Lyophilisation is widely used in pharmaceutical manufacturing, yet its role varies depending on the therapeutic class.
Common Freeze-Dried Pharmaceutical Products
- Vaccines requiring long-term stability
- Antibiotics and antiviral formulations
- Biologic injectables such as monoclonal antibodies
- Hormonal therapies and diagnostic kits.
Each application leverages freeze-drying’s ability to maintain potency and reduce the risk of contamination during storage. Additionally, the dry form often allows faster reconstitution, supporting clinical efficiency.
Comparing Liquid and Lyophilised Drug Forms
Image Courtesy of Freepik
To understand the practical value of freeze-drying, it is helpful to examine how it differs from traditional liquid formulations.
| Feature | Liquid Formulation | Lyophilised Formulation |
| Stability | Limited by moisture-driven reactions | Significantly improved shelf life |
| Storage conditions | Often requires a strict cold chain | Greater flexibility depending on the product |
| Transport efficiency | Higher weight and volume | Reduced weight and improved logistics |
| Reconstitution | Ready to use | Requires dilution before use |
| Risk of degradation | Higher during long storage | Lower due to minimal water content |
This comparison highlights why pharmaceutical developers frequently choose freeze-drying for sensitive compounds.
Advantages Beyond Shelf Life
While stability is the primary objective, lyophilisation offers broader operational benefits for the pharmaceutical sector.
Strategic Benefits for Manufacturers
- Enables global distribution without compromising product integrity
- Facilitates precise dosing through stable powder forms
- Supports extended product lifecycle management
- Enhances compatibility with sterile packaging processes.
Furthermore, freeze-drying can reduce reliance on preservatives, aligning with evolving regulatory expectations and patient safety standards.
Challenges and Process Considerations
Despite its advantages, lyophilisation presents technical and economic challenges. Equipment costs, process duration, and energy consumption can be significant. Therefore, manufacturers must carefully balance investment with product requirements.
Key Challenges to Address
- Complex process development and validation
- Sensitivity to formulation composition
- Risk of structural collapse if parameters are mismanaged
- Need for skilled operational oversight.
Nevertheless, advances in process analytics and equipment design continue to mitigate these limitations.
The Role of Formulation Science in Successful Freeze-Drying
Pharmaceutical lyophilisation is not solely about machinery; formulation plays an equally critical role. Stabilising excipients, such as sugars or amino acids, are often added to protect the active ingredient during freezing and drying. These components form a supportive matrix that prevents aggregation or denaturation.
Equally important is the reconstitution profile. A well-designed freeze-dried product dissolves quickly and uniformly, ensuring consistent dosing in clinical settings. Thus, collaboration between formulation scientists and process engineers remains central to successful product development.
Future Directions in Pharmaceutical Lyophilisation
As pharmaceutical innovation accelerates, the demand for reliable preservation technologies grows. Emerging therapies, including gene-based treatments and personalised biologics, are likely to rely heavily on freeze-drying techniques. Advances in automation, monitoring, and energy-efficient refrigeration systems are also expected to enhance process sustainability.
Furthermore, the integration of digital control systems enables real-time optimization, improving consistency while reducing waste. These developments indicate that lyophilisation will remain a critical enabler of modern drug delivery solutions.
Conclusion
Lyophilisation plays a pivotal role in preserving pharmaceutical products by removing moisture while maintaining structural integrity and therapeutic efficacy. From vaccines and biologics to diagnostic agents, freeze-drying supports stability, safety, and global accessibility. Although the process requires sophisticated equipment and expertise, its benefits in ensuring reliable treatment outcomes are undeniable. As pharmaceutical science continues to evolve, lyophilisation stands as both a proven preservation method and a platform for future innovation in drug development and distribution.